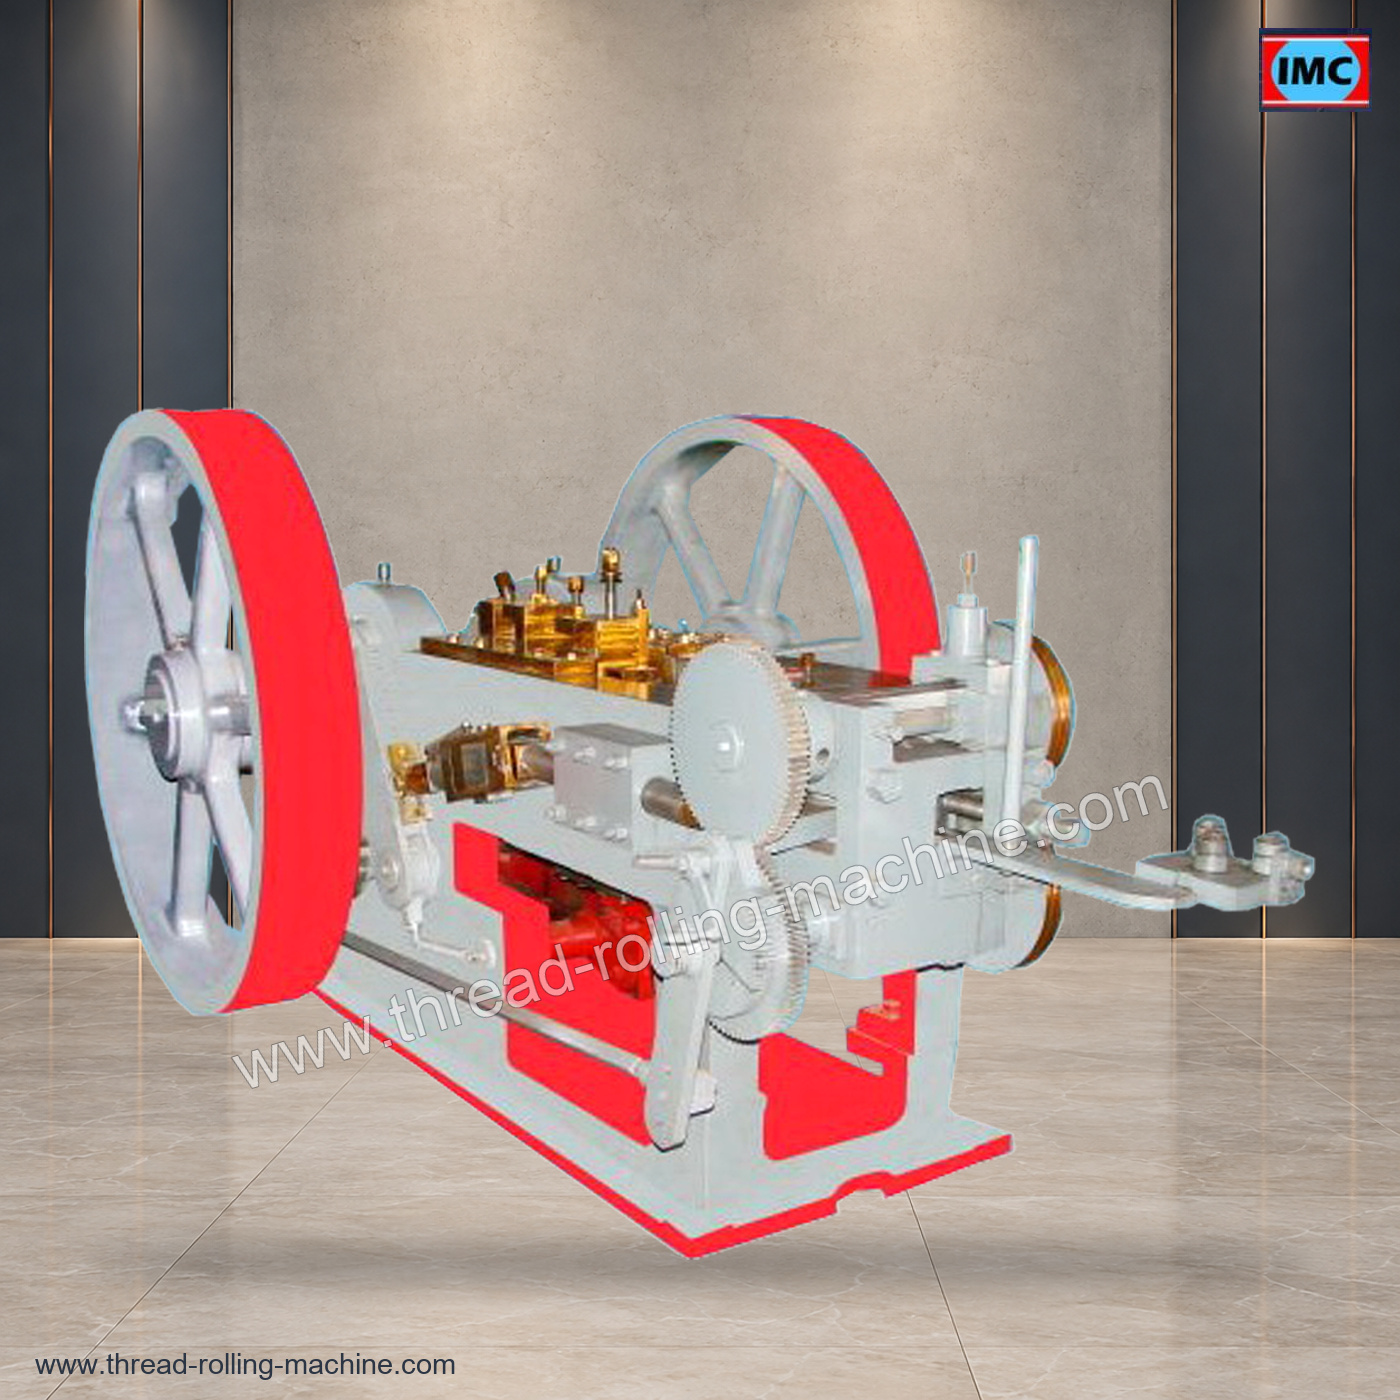
Automatic Cold Heading Machine
Cold heading forms a fastener head from a prepared blank using suitable tooling. The part geometry, material and forming sequence determine the machine and tooling arrangement to discuss.Information f ...
VIEW MOREIndustrial Machinery Corporation

No product-specific playlist is stored for this item yet. View IMC machine demonstrations and production videos in the main gallery.
Model data and technical details supplied for this product. Final configuration can be confirmed against your application.
| Model No. | Length Of Bolt | Dia. Of Bolt | Production Per Minute | Power Required (H.P x RPM) |
| IMC-HTM-1 | 1/2" - 1" | 80-85 | 80 - 90 | 1 x 1440 |
| IMC-CHM-2.5 | 1/2" - 2" | 70-75 | 60 - 80 | 3 x 1440 |
| IMC-CHM-3 | 3/4" - 3" | 60-65 | 50 - 60 | 5 x 1440 |
| IMC-CHM-4 | 1" - 4" | 45-50 | 40 - 45 | 7.5 x 1440 |
| IMC-CHM-5 | 1.5" - 5" | 35-40 | 30 - 35 | 15 x 1440 |
| IMC-CHM-6 | 2" - 6" | 25-30 | 25 - 30 | 20 x 1440 |
Send drawings of the incoming and finished parts, material grade and the dimensions to be changed. Identify whether both operations are required for each bolt.
Bolt head trimming and shank reducing are forming or finishing stages within a bolt production route. The required tooling must match the incoming blank and the finished head and shank dimensions.
Provide drawings of the incoming blank and finished bolt, including the head profile and shank dimensions. Ask which operations, dies and changeover parts are included for each bolt size.
Cold heading forms a fastener head from a prepared blank using suitable tooling. The part geometry, material and forming sequence determine the machine and tooling arrangement to discuss.Information f ...
VIEW MORE
Automatic cold thread rolling is used to form external threads on prepared blanks with matching dies. The required feeding arrangement and blank consistency are part of the machine selection.Informati ...
VIEW MORE